
www.technology4environment.com
18
'26
Written on Modified on
Energy-Efficient Circuit Breaker Manufacturing with ISO 50001
ABB's Senatobia facility combines geothermal heating, solar power and digital energy management to cut energy use in electrical equipment production.
global.abb
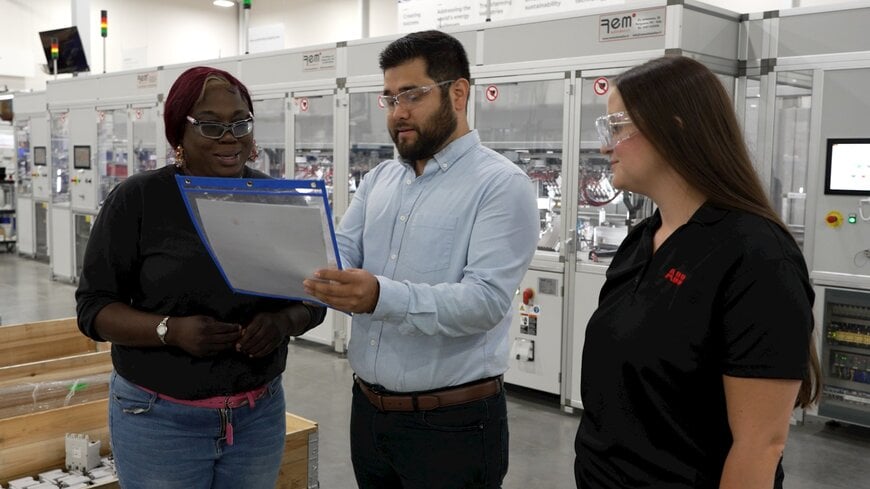
ABB's manufacturing facility in Senatobia, Mississippi, produces circuit breakers, switches and transfer switch assemblies for customers across North America. The site has become a reference for sustainable manufacturing within ABB, having reached the company's Mission to Zero environmental milestone in 2023 and gained ISO 50001 certification for energy management in 2024.
Energy Costs and Environmental Targets in Electrical Equipment Production
Manufacturers of low-voltage electrical equipment face a twofold challenge. Production sites consume significant energy for climate control, machinery and testing, while customers and investors increasingly expect suppliers to demonstrate measurable environmental performance. At Senatobia, the objective was to reduce environmental impact while improving manufacturing efficiency, treating energy and resource use as operating costs that can be engineered down rather than as fixed overheads.
Energy Management Technologies Deployed on Site
The facility combines several technologies. Geothermal heating and cooling uses the stable temperature of the ground to support climate control, lowering the energy required compared with conventional heating and air conditioning. On-site solar generation supplies renewable electricity, reducing dependence on the grid and supporting long-term energy resilience.
Digital energy management provides real-time monitoring of consumption across operations, allowing the team to identify efficiency gains continuously rather than through periodic audits. Lean manufacturing processes are applied to reduce material waste, and water management practices cover all operations on site.
ISO 50001 Energy Management System
ISO 50001 is the international standard for energy management systems. It requires an organisation to establish an energy baseline, set performance indicators and follow a plan-do-check-act cycle of continuous improvement. Certification therefore indicates that energy performance at Senatobia is measured and managed systematically, with the digital monitoring tools providing the data needed to track progress against defined indicators. Site employees are actively involved in advancing these energy and sustainability goals.
Operational Benefits and Customer Impact
According to ABB, the measures deliver competitive advantages as well as environmental gains. Higher energy efficiency reduces operating costs, waste reduction improves margins, and documented sustainability performance helps attract both talent and customers who expect responsible operations from their supply partners.
The benefits extend to the products leaving the plant. Circuit breakers, switches and transfer switch assemblies made at Senatobia are used by customers to manage power distribution more efficiently, from data centres optimising electrical infrastructure to manufacturing plants seeking to reduce their own energy consumption and emissions.
Next Steps with AI-Enabled Optimisation
The facility is continuing to invest in next-generation manufacturing technologies, including AI-enabled optimisation in 2026, designed to improve both production efficiency and environmental performance. ABB presents Senatobia as a model for how American manufacturing can remain globally competitive while meeting rising expectations on sustainability.
Edited by Natania Lyngdoh, Induportals editor, with AI assistance.
www.abb.com
